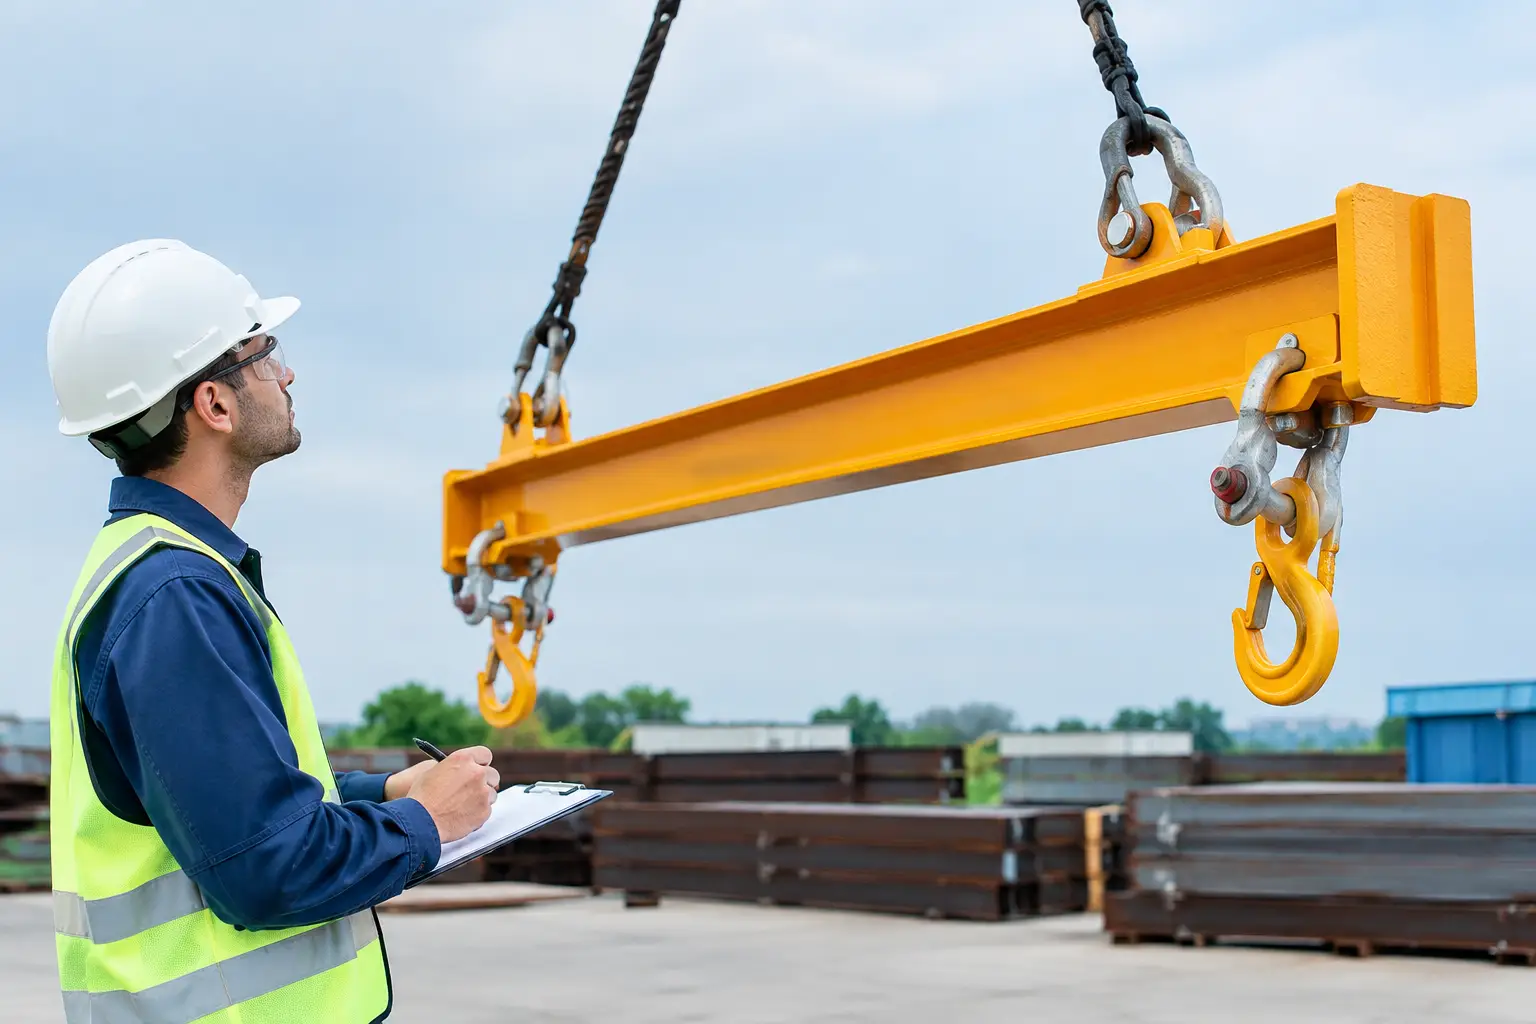
A wire rope termination can look secure and still be unsafe. Incorrect wire clip installation may allow a rope to slip under load, reduce its effective strength, damage the rope’s live end, or create a termination that cannot be properly inspected. For lifting, towing, and marine applications, the clip, rope, thimble, installation method, and certification requirements must be considered as one system.
Wire rope clips are useful for specified applications and temporary or field-made terminations. They are not a universal replacement for a professionally swaged socket, spelter socket, or factory-manufactured wire rope sling. The right choice depends on the duty, rope construction, load direction, expected service life, and applicable project or vessel requirements.
Start With the Correct Wire Clip
A wire clip must match the nominal diameter and construction of the wire rope. A clip that is oversized will not grip correctly. One that is undersized can crush strands, distort the rope, and make correct installation impossible. Confirm the clip’s marked size, manufacturer rating, material grade, and intended use before work begins.
For general wire rope applications, common clip designs include U-bolt clips, fist-grip clips, and forged clips. U-bolt clips are widely used, but the U-bolt bears on one side of the rope and installation direction is critical. Fist-grip clips apply force more evenly across both rope parts and can be advantageous where the termination will remain in service. Selection still needs to follow the manufacturer’s instructions and the governing standard for the job.
Material compatibility matters in marine and offshore environments. Galvanized wire rope, stainless steel wire rope, galvanized clips, and stainless steel clips have different corrosion behavior and service limits. A mixed-material assembly may be acceptable in some controlled uses, but it can introduce corrosion risk and should not be selected by appearance alone.
Before fitting clips, inspect the rope section to be terminated. Reject rope with severe corrosion, broken wires, flattening, kinks, birdcaging, heat damage, or visible core displacement. Clips cannot restore capacity to a damaged rope.
When Wire Clips Are Not the Right Termination
Wire rope clips have limitations. For critical lifting eyes, personnel-related applications, high-cycle lifting, long-term marine service, or assemblies that require a defined rated capacity, a swaged eye with the correct ferrule and thimble is often the better solution. A professionally processed termination provides a controlled result, traceable dimensions, and, where required, load-test certification.
Wire clips should also be approached cautiously on rotation-resistant, non-rotating, compacted, or plastic-filled wire ropes. These constructions can respond differently to localized clamping force. The rope manufacturer’s instructions take priority. If a lifting plan, client specification, class requirement, or local regulation prohibits clip terminations, do not treat field convenience as an exception.
The practical question is not simply whether a clip can hold the rope. It is whether the completed termination is suitable for the load, consequence of failure, inspection regime, and documentation required for the work.
Wire Clip Installation Procedure
Prepare the eye before installing the first clip. Form the rope around a correctly sized thimble where the application requires one. The thimble protects the eye from pinching and abrasion and helps maintain the proper bend radius. Avoid sharp bends and do not force a thimble that is too large or too small for the rope and eye geometry.
Place the First Clip Correctly
For a U-bolt wire rope clip, follow the established rule: never saddle a dead horse. The saddle goes on the live end, which is the load-bearing side of the wire rope. The U-bolt goes over the dead end, also called the short or tail end.
This orientation matters because the saddle distributes clamping force over the live end. Reversing the clip can damage the load-bearing section and reduce holding performance. Mark the live end before installation if there is any chance the crew could confuse the two sides.
Position the first clip close to the dead end, while maintaining the clearance specified by the clip manufacturer. Do not place it directly on the thimble unless the manufacturer’s instructions specifically show that arrangement.
Fit the Remaining Clips at the Specified Spacing
The number of clips, their spacing, and the required tail length depend on rope diameter, clip design, and governing standard. Do not use a rule of thumb such as “three clips for every rope.” A termination that works on a small utility rope may be wholly unsuitable for a larger lifting line.
Install the remaining clips in the same orientation, at uniform spacing specified by the manufacturer. Uneven spacing can concentrate load and make it difficult to inspect the assembly. Ensure each saddle remains on the live end throughout the sequence.
Where a turnback eye is installed around a thimble, maintain the specified dead-end length beyond the final clip. Cutting the tail too short removes a visible inspection point and can compromise the termination’s intended grip arrangement.
Tighten to the Required Torque
Tighten the nuts evenly, alternating between them to keep the saddle seated squarely. Use a calibrated torque wrench where the manufacturer specifies a torque value. Tightening by feel is not a controlled installation method, especially for lifting or safety-critical work.
Under-tightening can allow rope movement and slip. Over-tightening can crush the rope, deform strands, and reduce service life. Torque values differ by clip size, material, thread condition, and manufacturer. Use the applicable data for the exact clip, not a generic table from another product.
After initial tightening, apply a controlled proof load only when permitted by the relevant procedure or project requirement. Recheck torque after the rope has seated under load. In service, clips can require retightening because wire rope settles and slightly changes shape after loading.
Inspection Points Before Release to Service
A completed clip termination should be visually checked by a competent person before it is used. Confirm that the clips are the correct size and type, all saddles face the live end, nuts are fully engaged, spacing is even, and the required tail length remains visible.
Check the rope around the clips and thimble for crushing, strand displacement, sharp bends, or contact damage. Also inspect the thimble for distortion and make sure the eye is not twisted. If the assembly will be used in a marine setting, check that the selected components are suitable for expected corrosion exposure and that drainage will not be trapped around the termination.
For controlled lifting operations, records should identify the rope specification, clip type and quantity, installation date, installer, inspection status, and any test result. Documentation is not paperwork for its own sake. It gives lifting supervisors, vessel crews, and maintenance teams a clear basis for deciding whether the assembly remains fit for service.
Common Installation Failures
Most failures are preventable. Reversed U-bolt clips are among the most common errors, followed by incorrect clip sizes, missing clips, insufficient tail length, and nuts tightened without torque control. Another frequent issue is reusing clips after they have been removed from a loaded termination. Reuse may not be permitted, particularly when threads, nuts, saddles, or U-bolts show wear, corrosion, deformation, or uncertain history.
Field modifications also create risk. Do not add clips to compensate for a poorly formed eye, install clips over damaged rope, or mix unmatched clip brands and sizes in one termination. A larger number of incorrectly installed clips does not create a compliant assembly.
Build the Termination Around the Job
For temporary guying, noncritical restraint, and approved utility work, correctly installed wire rope clips can be practical and serviceable. For rated lifting slings, crane falls, critical towing arrangements, and demanding marine use, a cut-and-swaged assembly or engineered termination is generally the more controlled route.
C&C International supports wire rope processing, swaging, load testing, documentation, and onsite rigging requirements for projects that cannot rely on assumptions. Providing the rope diameter, construction, intended load, eye configuration, environment, and required certification at the planning stage allows the termination to be built for the actual job.
A wire rope clip is a small component with a large consequence. Treat its installation as a defined technical task, verify it before loading, and select a processed termination whenever the application demands higher assurance.