A wire rope assembly rarely fails because the rope was selected without care. More often, the weak point is at the end: an incorrectly fitted socket, a poorly positioned clip, a damaged eye, or a termination that was never verified after installation. This steel rope termination guide addresses the decisions that determine whether a finished assembly is suitable for lifting, restraint, towing, mooring, or marine service.
The correct termination is not simply the one that fits the available hardware. It must match the rope construction, diameter, grade, coating, loading direction, design factor, and duty cycle. It must also be processed and documented in a way that supports the site’s inspection and compliance requirements.
Start With the Rope and the Job
Before choosing a socket, ferrule, or clip, confirm the rope’s full specification. Record the nominal diameter, construction, core type, lay direction, tensile grade, finish, and minimum breaking force. These details affect compatibility and the retained efficiency of the finished termination.
A rotation-resistant lifting rope, for example, requires different handling from a general-purpose 6-strand rope. A galvanized wire rope working near saltwater has different corrosion considerations from an ungalvanized rope installed in a protected plant environment. If the rope has been in service, its condition must be assessed before it is cut or reterminated. Broken wires, corrosion, crushing, heat damage, and diameter reduction can make retermination unsuitable regardless of how sound the new end fitting appears.
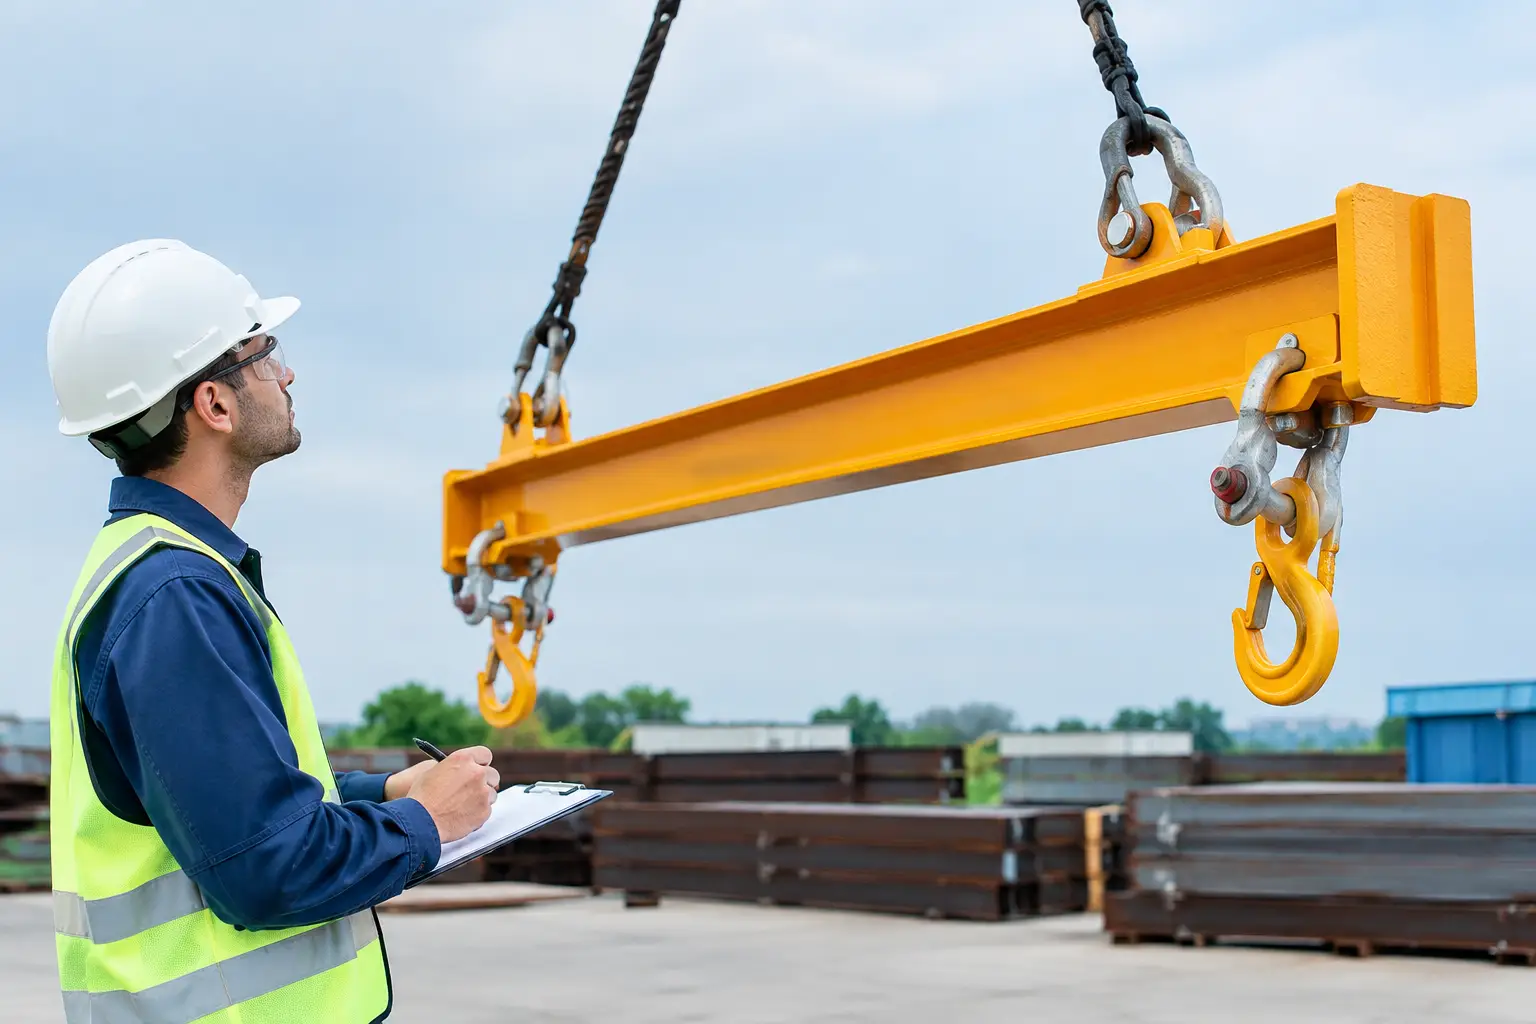
The application also matters. A lifting sling eye needs controlled geometry and a known working load limit. A wedge socket on a crane line needs correct dead-end orientation, adequate tail length, and inspection access. A marine mooring or towing arrangement may prioritize fatigue resistance, abrasion protection, and compatibility with thimbles or connecting hardware. There is no universal termination method that performs best in every role.
Define the Load Path
Specify where load enters and leaves the assembly. Identify whether loading is straight, angled, intermittent, shock-prone, or subject to repeated cycling. Side loading on a thimble, socket, shackle, or hook can reduce service life even when the wire rope itself is correctly selected.
Also distinguish between a permanent manufactured assembly and a field-adjustable arrangement. Permanent terminations generally provide greater control over geometry and traceability. Field-installed clips and wedge sockets can be practical where adjustment or replacement is required, but they demand disciplined installation and follow-up inspection.
Steel Rope Termination Guide: Choosing the Method
The termination method should be selected from the rope manufacturer’s recommendations, the hardware manufacturer’s instructions, and the applicable lifting or marine requirements. Four common options serve distinct purposes:
- Swaged ferrules and sleeves create compact, permanent eyes or fittings. A correctly sized ferrule is pressed using calibrated equipment and the specified die profile. This is widely used for lifting slings, safety lines, structural support, and engineered assemblies where repeatable production and documentation are required.
- Poured sockets use resin or zinc-based socketing systems to develop a high-strength termination. They are common on larger ropes, crane pendants, bridge cables, and demanding marine or industrial applications. Socket preparation, brooming, cleaning, temperature control, and curing are critical to performance.
- Wedge sockets provide a removable, adjustable termination for appropriate running-rope applications. Correct installation depends on the approved wedge, socket, rope size range, dead-end arrangement, and a properly secured tail. They should not be treated as a shortcut for every lifting connection.
- Wire rope clips can form eyes or secure dead ends where permitted, particularly for static or temporary duties. Their efficiency is usually lower than a properly swaged or socketed assembly, and installation errors are common. Clip quantity, spacing, torque, retorque requirements, and orientation must follow the clip manufacturer’s instructions.
Hand splicing may also be appropriate for selected rope constructions and specialist applications, but it is not interchangeable with a mechanical swage or socket. The retained strength, dimensions, inspection criteria, and competency requirements must be evaluated for the exact rope and intended service.
Why Clips Need Extra Discipline
Wire rope clips are familiar hardware, which can lead crews to underestimate the risks. A clip that is undersized, mismatched to the rope construction, installed backwards, or left unretorqued can allow slippage or crush the rope at the wrong point.
For conventional U-bolt clips, the saddle is generally positioned on the live end of the rope, not the dead end. This is commonly remembered as “never saddle a dead horse.” The phrase is useful, but it does not replace the manufacturer’s installation table. Do not assume the number of clips or the required tightening torque from past jobs. Both vary by clip type and rope diameter.
After the assembly has been loaded, clips should be reinspected and retightened where required. This is particularly relevant after initial bedding-in, vibration, or transport to site. If the assembly is for personnel lifting, critical lifting, or another high-consequence duty, confirm whether clips are permitted at all under the applicable procedure.
Control the Fabrication Process
A reliable termination starts with proper rope handling. Cut the rope using a method that prevents the strands from opening or distorting. Apply seizing where necessary, maintain the rope’s lay, and avoid heat damage to coatings or the core. The eye size must suit the thimble or connection hardware without forcing the rope into an excessively tight bend.
For swaged assemblies, verify the ferrule material, bore size, die set, press capacity, and final pressed dimensions. A press alone does not prove a swage is correct. The operator must measure the finished ferrule against the approved criteria and inspect for cracks, uneven compression, strand damage, or incorrect eye geometry.
For socketed assemblies, surface preparation is equally important. Lubricant, moisture, debris, or incomplete brooming can affect bonding and load transfer. The socket must be compatible with the rope diameter and construction, and the compound or metal-pouring process must follow its specified preparation and cure requirements.
Where the application calls for proof loading or load testing, perform it on the completed assembly, not on individual components only. The test should be supported by identification, results, date, inspection details, and traceable certification. For engineered or project-specific work, PE-endorsed documentation may be required.
Inspect Before Dispatch and During Service
A new termination deserves the same scrutiny as a rope that has been in operation for months. Confirm that the assembly identification is legible, the eye and thimble are correctly seated, and the hardware pin or connection is appropriate for the intended load path. Check that no sharp edges, weld spatter, or poorly aligned fittings can chafe the rope.
In service, inspect the termination zone closely. The rope often deteriorates first where it enters a socket, passes around a thimble, or bears against hardware. Look for broken wires, localized corrosion, birdcaging, flattening, abrasion, displaced clips, ferrule cracking, socket movement, or a change in eye shape.
Inspection frequency depends on use. A stored spare sling may need periodic condition checks, while a crane line, offshore lifting assembly, or vessel equipment exposed to salt spray and repeated load cycles needs a more rigorous regime. Remove equipment from service when damage exceeds the applicable rejection criteria or when its history cannot be confirmed.
Specify a Job-Ready Assembly
Procurement descriptions should state more than “wire rope with eye.” Include the rope type and diameter, finished length, termination type at each end, thimble requirement, hardware connection, working load limit or minimum breaking force basis, certification requirement, and intended application. If the assembly will be installed in a constrained location, provide drawings, connection dimensions, and any site handling limitations.
This level of detail allows a technical supplier to cut and swage to spec, select compatible hardware, complete load testing where required, and issue full documentation. It also prevents a common site problem: receiving a correctly rated rope that cannot be connected because the eye, socket, shackle, or hook geometry was not coordinated.
For urgent marine and industrial work, C&C International can support wire rope processing, testing, documentation, and onsite rigging requirements as part of a complete equipment scope. Early review is especially valuable when the assembly is nonstandard, safety-critical, or exposed to harsh operating conditions.
The best time to resolve a termination question is before the rope is cut. Bring the rope data, load case, connection details, and certification requirements together at the specification stage, and the finished assembly can arrive ready for controlled, accountable service.