A wire rope termination can determine whether an assembly is fit for a routine restraint duty or a safety-critical lift. When assessing wire clips versus sockets, the question is not simply which fitting costs less or installs faster. It is whether the termination method delivers the required efficiency, fatigue performance, inspection access, documentation, and service life for the load and operating environment.
Wire rope clips and sockets both have established roles in marine, lifting, towing, and industrial work. They are not interchangeable. A selection made without reference to rope construction, loading pattern, applicable standards, and manufacturer instructions can reduce the assembly’s rated capacity or create an inspection issue later in service.
What Wire Rope Clips Are Designed to Do
Wire rope clips, often called U-bolt clips or wire rope clamps, secure a loop by clamping the dead end of a wire rope against its live end. The arrangement is generally used with a thimble where the eye needs protection from crushing and abrasion.
Their main practical advantage is field installation. Clips can be fitted using ordinary hand tools, making them useful for temporary guy lines, restraint lines, light-duty applications, and certain noncritical rigging arrangements. They also allow an assembly to be adjusted or removed without cutting off a permanent termination.
That convenience comes with limits. The rope is bent sharply around the thimble, then compressed under the clip saddle and U-bolt. This affects the rope’s efficiency and can make the assembly less suitable for dynamic loading, repeated high-load cycles, or critical lifting duties. Correct clip type, number of clips, spacing, torque, rope diameter, and installation orientation must follow the clip manufacturer’s instructions and the applicable standard.
The familiar instruction to place the saddle on the live end is still relevant, but it is not enough on its own. Mixing clip sizes, using worn or mismatched hardware, failing to re-torque after initial loading, or leaving too short a dead end can compromise the connection. Clips should never be treated as a universal shortcut for forming a lifting eye.
What a Socket Termination Provides
A socket termination transfers load from wire rope into a purpose-designed fitting. The socket can be attached by swaging, resin socketing, or zinc socketing, depending on the rope, application, specification, and approved process. Wedge sockets are another category and provide a removable mechanical termination, commonly used where reeving or replacement is required.
For permanent or high-capacity assemblies, a properly made socket generally offers a more controlled and efficient termination than a clipped eye. It is common in crane hoist ropes, mooring pendant assemblies, towing connections, structural tension systems, and engineered lifting arrangements. The socket body also provides a defined connection point for shackles, pins, hooks, or other rated hardware.
Socketing is not merely a matter of inserting rope into a fitting. The rope must be prepared correctly, the socket must match the rope diameter and construction, and the termination must be produced to the approved procedure. Resin and zinc systems require particular control over rope brooming, cleaning, socket alignment, pouring conditions, cure time, and final inspection. Swaged sockets require correct dies, calibrated equipment, and dimensional verification after pressing.
Where documented capacity is required, the completed assembly may also need proof loading and certification. This is especially relevant when the rope is part of a lifting system, a critical towing connection, or a project package subject to client, class, or regulatory requirements.
Wire Clips Versus Sockets: The Operational Difference
The most useful comparison is not clips against sockets in the abstract. It is a comparison of duty, consequence of failure, and control of the finished assembly.
Wire clips are adaptable and readily installed on site. They can suit noncritical static work where the load case is understood, the assembly can be inspected frequently, and the installation follows the manufacturer’s data. They may also be selected where a temporary eye is needed and permanent processing is not justified.
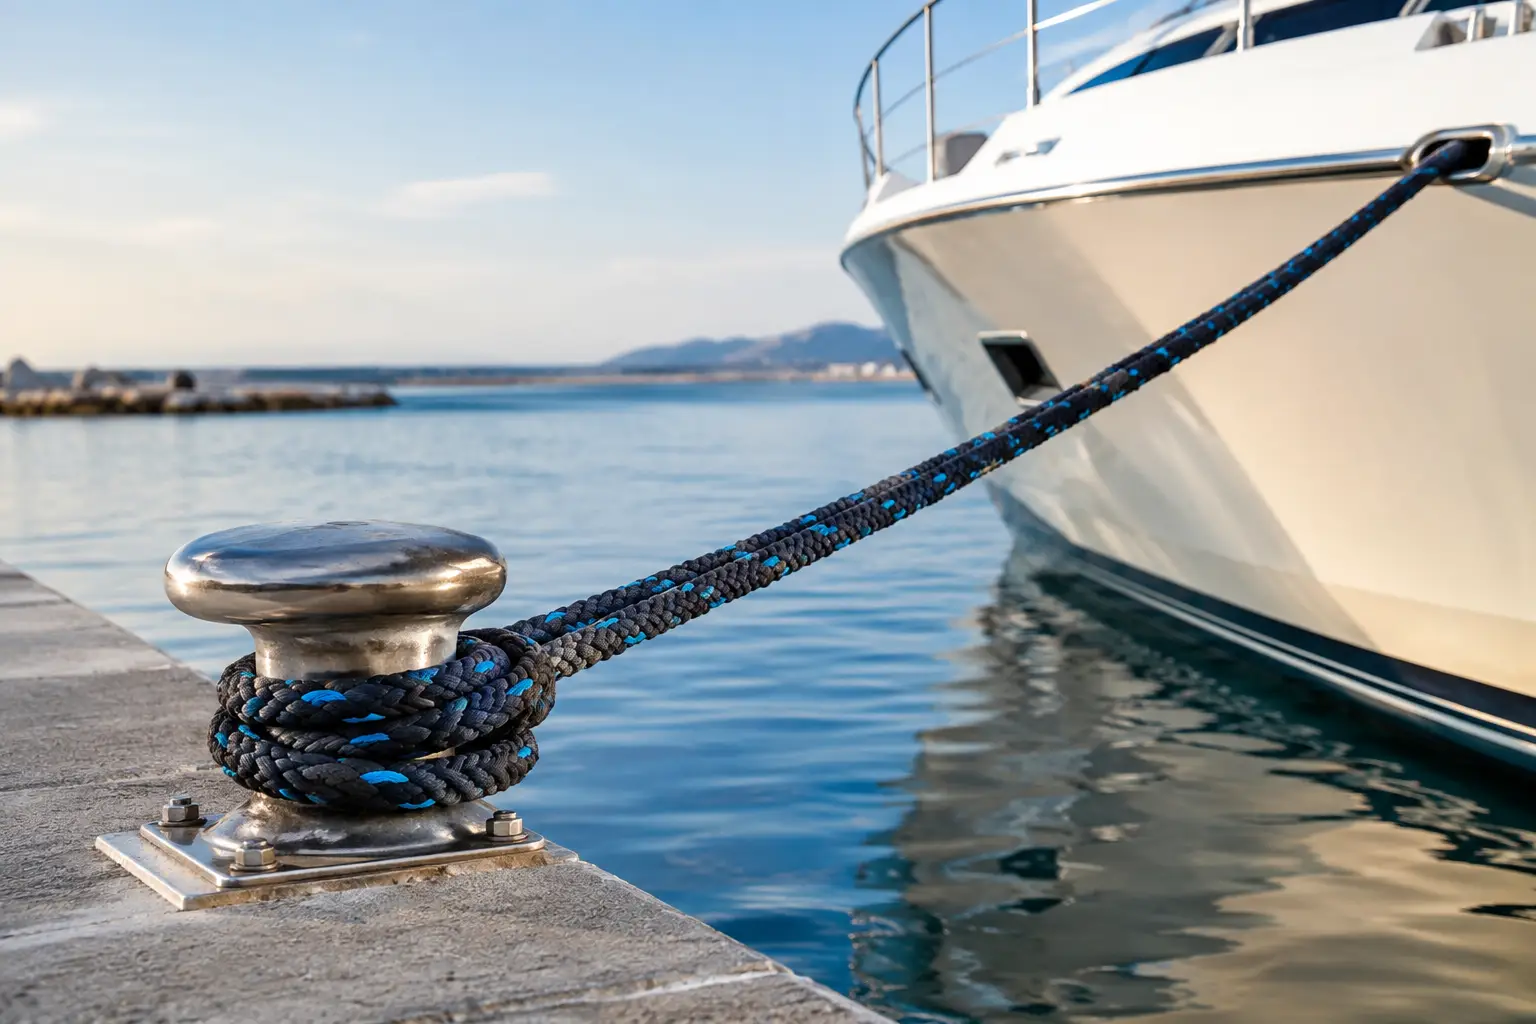
Sockets are generally selected when the rope assembly must deliver predictable capacity, a compact termination, repeatable fabrication quality, and traceable documentation. They are better suited to demanding load paths, including lifting, marine towing, mooring, and engineered tensioning applications. The initial cost and processing time are higher, but the termination is built around the duty rather than adapted in the field.
Neither option removes the need to consider the rope itself. A rotation-resistant crane rope, for example, has different termination requirements from a six-strand general-purpose wire rope. A rope operating through sheaves, exposed to saltwater, or loaded in repeated cycles requires a different assessment from a static barrier line. The right answer depends on the complete assembly, not the termination alone.
Strength Efficiency and Dynamic Service
A wire rope’s minimum breaking force does not automatically become the capacity of its finished assembly. Bending the rope into an eye, clamping it with clips, or terminating it in a socket all affect performance. The manufacturer’s stated termination efficiency and the applicable design factor should be used when establishing the working load limit.
Dynamic service deserves particular attention. Shock loading, vessel movement, snatch loads, crane acceleration, and vibration can cause a termination to behave very differently from one under steady tension. Clip nuts may loosen if not installed and maintained correctly. The rope can settle after loading, requiring re-torque. Repeated bending at an eye can also accelerate fatigue damage.
A professionally socketed termination is usually the more appropriate choice where load cycles are frequent, load consequences are high, or the assembly is part of a certified lifting arrangement. That does not mean every socket is automatically suitable. Incorrect socket geometry, poor preparation, incompatible resin, or an unapproved fabrication process can defeat the purpose of specifying a socket.
Inspection Requirements in Service
Wire clips make visual inspection relatively straightforward because the rope, thimble, nuts, and saddle are exposed. Inspectors should look for loose nuts, deformation, corrosion, broken wires near the eye, slippage, thimble damage, and insufficient dead-end length. Any movement of the live end through the clips is a serious warning sign.
Sockets require a different inspection approach. Check for cracking, corrosion, distortion, worn pins, damaged locking arrangements, and wire breaks where the rope exits the socket. The rope entry point is critical because fatigue and corrosion can develop in this transition area. For poured sockets, the socket body and the visible rope interface should be examined for signs of movement or distress.
Inspection intervals should reflect the service condition, not just the calendar. Offshore exposure, abrasive cargo operations, frequent lifting cycles, and corrosive marine environments justify closer attention. Records should identify the rope, fitting, fabrication date, proof-load information where applicable, and inspection findings. Traceability is valuable when an assembly must be removed, replaced, or investigated after an incident.
Selecting the Right Termination for the Job
Start with the application. Is the assembly intended for lifting personnel-sensitive loads, securing cargo, supporting a static structure, towing equipment, or handling a vessel mooring load? Then confirm the rope type, nominal diameter, grade, construction, expected loading, environmental exposure, connection hardware, and required certification.
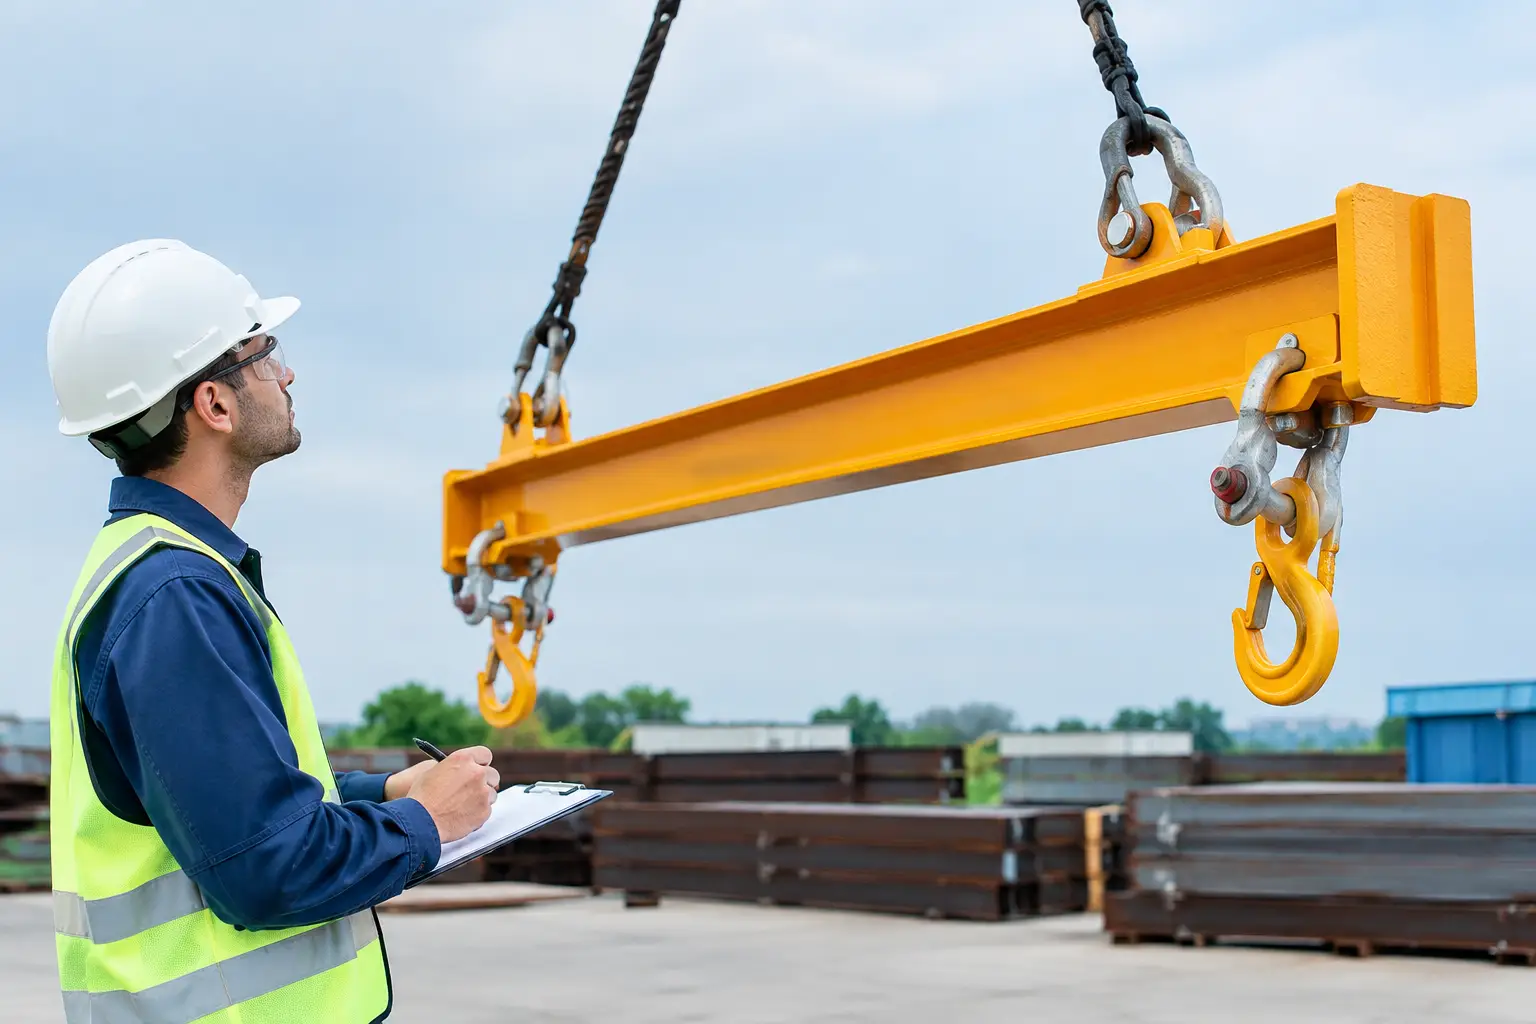
For a temporary noncritical restraint, a correctly installed clip termination may be appropriate. For a lifting sling, crane pendant, offshore towing bridle, or wire rope assembly carrying a specified working load limit, a purpose-made socketed or swaged termination is often the more defensible engineering choice.
Procurement teams should avoid ordering only by rope diameter and fitting name. A request for a “wire rope with socket” should state the required rope construction, finished length, socket type, eye or pin size, desired connection hardware, load requirement, certification need, and service environment. This prevents a technically correct component from becoming an unsuitable assembly once it reaches site.
C&C International can cut and swage wire rope to specification, coordinate load testing where required, and provide documentation aligned with the project scope. For specialized assemblies, early technical review helps identify whether a clip termination, a swaged socket, a poured socket, or another engineered end connection is appropriate before fabrication begins.
The best termination is the one that matches the load case, the rope, and the consequences of failure. Specify it with the same discipline applied to the rope and lifting hardware around it.